In this article we will discuss the main elements of equipment for craft beer production and the minimum requirements to meet brewing technology standards.
In order not to complicate the subject further, we will focus on small factories with a capacity of 250lt to 2,000lt per batch.
Nowadays, there are several configurations for the design of a cooking room, which can be summarized as follows:
Cooking room with separate filtering tank, of German tradition.
This type of design is of English tradition. In the past, a maceration of infusion used to be done by preheating the water and without further heating the pot.
Here are some examples to understand the various configurations:

Slowbeer 250 - German system

Slowbeer 500 Plus - English system

Slowbeer 250 Plus - English system
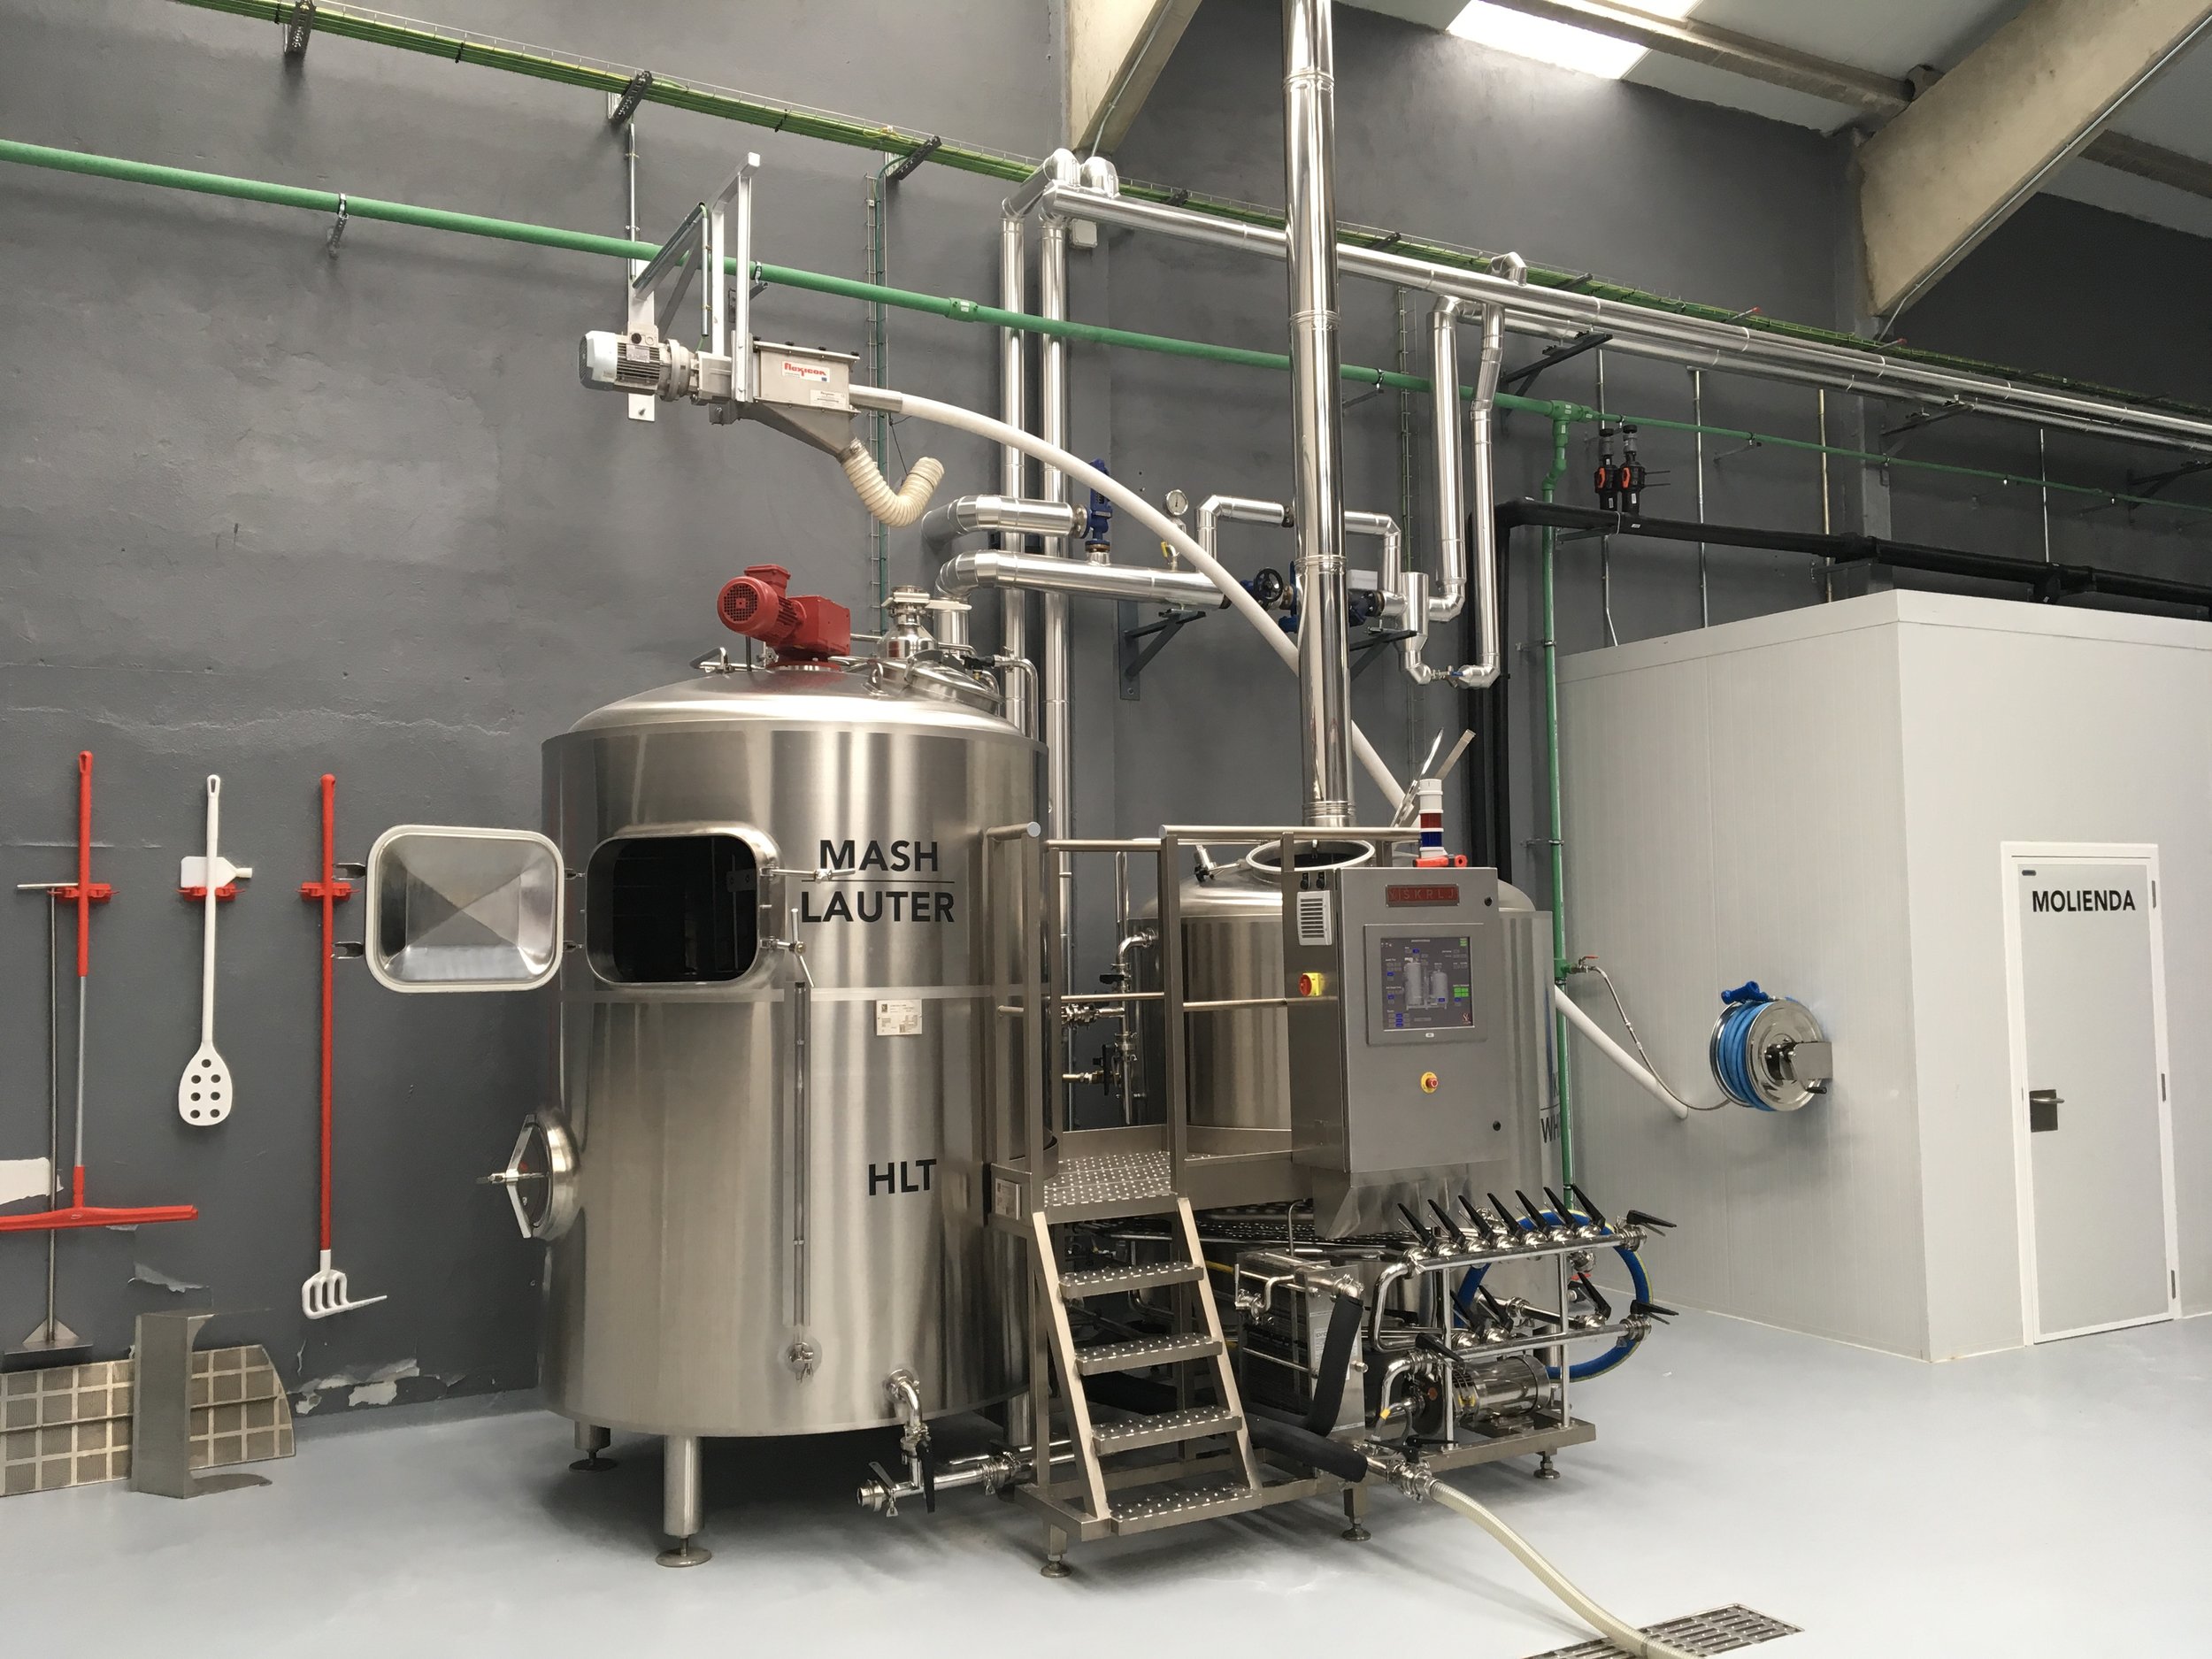
Slowbeer plus 10/20/25HL - English system
The type of equipment design mainly influences the brewing time and the quality of the wort. As can be seen in the examples, lauter tuns do not usually have a heating system, they only have temperature insulation.
The advantage of the English system over the German system is the possibility of continuous boiling, as soon as the lautering is finished and the wort is transferred to the boiling kettle, it is possible to brew a new batch in the mash kettle. This process is possible thanks to the simultaneous heating of the 2 pots.
Here are the production times for 2 consecutive processes (double cooking):
German 2-vessel brewhouse: 11 hours —> Slowbeer 250 brewhouse
English-style 2-tank brewhouse: 8.5 hours —> Slowbeer 250 plus, Slowbeer 500 Plus, Slowbeer Plus 10/20/25HL
German cooking room with 3 vats: 10 hours Firing room 1000
German 4-tank brewhouse: 6 hours 40HL brewhouse
Before we get into dimensions and heating methods, here are the main components of a traditional cooking room:
Heated mash tun: temperature control (probe and thermostat), stirrer, lid
Filtering tank with double filtering bottom and accessory for washing grains
Boiling vat (can be the same macerator)
Process pump with variable speed drive
Heat exchanger
Control panel
All components in contact with the product must be made of AISI 304 or AISI 316 stainless steel, in accordance with European regulations. To ensure greater product durability, it is recommended that the support structure and other components also be made of the same type of stainless steel. Other metals can easily cause poorly maintained stainless steel to rust, thereby reducing the equipment’s service life.
MASH TUN

In the mash tun, the malt is mixed with hot water (from a hot water tank or heated in the same kettle) to a temperature that allows the enzymes to transform the starches into sugars and create the wort.
The hot water tank typically has at least twice the capacity of the cooking chamber (for example, slowbeer 250, 600-liter water tank). The water from the tank is used for mash-in, washing, and alkaline cleaning.
Some brewhouses have a hopper equipped with a malt hydration system prior to mash-in. This process prevents dust from forming (which can lead to yield losses), avoids degrading the enzymes by keeping the temperature pre-mash that is too high, and prevents the formation of clumps.
Water-malt ratio and volume
The volume of the mash tun must be determined by considering the possible water-to-malt ratios, ranging from 1.6 L/kg for denser mashes to 5 L/kg for lighter, easier-to-manage mashes. If the mash tun is also used as the boil kettle, additional headspace must be allowed for due to the overboil of the wort. It is also important to note that many brewhouses have a number in their name (e.g., Slowbeer 250) that indicates the number of liters of wort to be brewed; this number is always related to the degree Plato of the wort produced (e.g., 250 liters at 17° Plato). When brewing beers with lower specific gravity, we’ll get more liters; for denser beers, we’ll get fewer liters.
Regardless of the heating method, this kettle must be equipped with a stirrer that can ensure uniform temperature distribution and promote enzymatic conversion (mash yield). The stirrer must not touch the sides or bottom of the kettle to avoid crushing the grain hulls. It is recommended that the paddle speed not exceed 2 m/s. Having a variable-speed drive on the agitator can aid the process depending on the type of mash tun you have; this is the case with our Slowbeer 500 Plus.
There are 3 main mashing techniques in brewing:
Infusion mash, no need to heat the mash pot.

Stepwise mashing, the wort is brought to certain temperatures for various enzyme activities
Decoction, a traditional Central European technique whereby one third of the mash is brought to a boil and then returned to the mash pot, increasing the temperature to the next step (this process can be repeated several times).
When designing a kitchen, you may want to consider whether to include the option to work with all three techniques, as in our cooking studios Plus.
There are several ways to heat a pot; nowadays, this is a very sensitive issue due to rising costs for gas and electricity.
The options available today are mainly 3:
Direct call
Electricity
Dry steam
1) The first one is the oldest one used, the flame distribution technology has improved a lot in the last years and the problems of caramelization of the wort have been partly overcome. In these types of equipment the stirrer has a fundamental task, since it avoids the burns of the skins at the bottom of the pot and that is why it has to be used continuously during the mashing process. These types of equipment are usually more economical, but they have limitations in certain contexts and alter the quality of the wort.

2) Electric equipment is divided into equipment with immersion heaters, equipment with heaters at the bottom of the pan and equipment with diathermic oil.
The first ones are not very advisable for professional equipment of this size 250/500lt, they have 2 main problems: the must caramelization/caramelization and the difficulty in cleaning.
The technology with contact resistors is applicable in small systems, less than 300lt.
The latest technology has a long history of use in the food industry and some brands use it in the brewing industry. The diathermic oil is heated in an external tank and recirculated through the jackets of the pots.
Electric equipment is recommended for beer production systems up to 500lt.
3) For volumes of 500 liters or more, the most commonly used heating method is dry steam. Dry steam can be produced using a boiler fueled by gas, diesel, electricity, or pellets. The steam reaches the brewhouse and, via a manifold, is distributed to the mashing and boiling kettles.
It is currently the most efficient and economical form of heating, however in some situations this choice is not the most appropriate:
When the firing rooms are small 250/500lt the cost of the boiler, steam installation, boiler room and certification can be higher than the firing room itself.
When the size or location of the premises does not allow us to install the boiler system.
FILTER TANK
After finishing the mash, the solid part must be separated from the liquid, trying to extract as many sugars as possible without dragging the cereal husks and extracting the tannins (astringent component). The design of the filter is essential so that the flow is continuous and does not allow undissolved particles to pass through.

This part of the process is called lautering and consists of two parts: filtering by recirculating the wort through the grains (this yields the first wort) and rinsing the grains (sparging) to extract as much sugar as possible (this yields the second wort). When this operation is performed in a dedicated kettle, it is called lauter tun; if it is carried out in the same mash tun, it is called mash filter.
The diameter of the lauter tun must be large enough to distribute the wort flow over the whole double-bottom, normally the height of the grain bed does not exceed 50cm. A false bottom is positioned a few centimeters above the bottom of the pot, usually made by water cuts of 0.7mmx80mm that occupy 10% of the total surface of the filter.
Some pots are equipped with lag-cutting paddles that favor the flow of the wort.
The wort is recirculated until it is clean, producing a clean wort means obtaining a more stable beer with more defined flavors.
The recirculation is done through a spray arm that may have one or more terminals such as plates, perforated balls or other diffusers.
Once the clean must is obtained, water at a temperature between 71 and 78ºC is added through the same spray arm. Adding water with a "shower effect" avoids the formation of preferential channels.
During this phase of the process it is important to always leave the grain bed covered to avoid excessive oxidation.
Filter vats usually have a rectangular manhole for bagasse discharge.
BOILING VAT
The boiling vat must have a volume large enough to contain the amount of pre-boiled wort, plus extra space for overboiling.
In this part of the process the must is brought to 100º with the following objectives:
Isomerization of alpha acids
Must sterilization
Deactivating enzymes
Coagulate and remove proteins
Evaporation of volatile defects
In smaller units, the boiling kettle is equipped with a tangential inlet for performing whirlpool—a clarification technique that generates a centripetal force, causing the heavier substances (proteins, polyphenols, and other poorly soluble compounds) to accumulate in the center of the kettle. The clarified wort is drawn off from the side of the kettle and passes through a heat exchanger.
The ways of heating the boiling pot are the same as for heating the mash tun with open flame, electrically or with dry steam. In case of steam or diathermic oil jackets an asymmetric design of the jackets is advisable to favor convective movements, it is advisable to apply the jacket.
PROCESS PUMP
The process manifold pump is one of the system’s main components. It is recommended that the parts in contact with the wort be made of 316 AISI , that the pump be equipped with a variable-frequency drive to adjust the speed at each stage of the process, and that it be capable of withstanding high temperatures.
The pump is used to transfer liquid from one pot to another, to perform the whirlpool and to transfer the wort to the fermenters.
HEAT EXCHANGER
In equipment of this size, a plate heat exchanger is usually installed. The cooling system is composed of several plates that favor the thermal exchange between the hot wort at 100º and the cooling water.

There are 2 types of plate heat exchangers:
1 stage, exchange between wort and water coming from the network or from a cold water tank. (Example. Wort cooling 100ºC -> 18ºC, Water heating 13ºC->83ºC)
2 stages: Stage 1, exchange between wort and water coming from the network or from a cold water tank. (Example. Wort cooling 100ºC -> 20ºC, water heating 13ºC->85ºC). Stage 2 exchange between wort and glycol (Example: Wort cooling 20ºC -> 7ºC, Water heating 1ºC->13ºC).
CONTROL PANEL
The various processes can be controlled from the control panel:
Temperature control
Stepwise maceration programming
Activate the pump and control its speed
Activate the agitator
Start a production cycle
The more technologically advanced equipment can control other parameters as well as interact with the water tanks.
The design of brewing equipment can be tedious, especially when it comes to defining dimensions, volumes and energy transfers.
One of the aspects our customers appreciate most is the performance of our equipment (brewhouse efficiency), which is around 90%, depending on the recipe.
We will discuss this concept in more detail in another article in the Processing category.
Here are the European standards that our brewing machinery complies with:

Directive 2006/42 CE Machinery Directive
Directive 2006/95/ CE : Low-Voltage Directive
Directive 2004/108/CE : Electromagnetic Compatibility
UNI EN ISO t Standard 12100-1:2005 General Principles for Design
UNI EN ISO n Standard 12100-2:2005 General Principles for Design
UNI EN ISO Standard 13857: Machine Safety
UNI EN ISO n Standard 13849-1:2007 General Principles for Design
Standard EN 983: Safety of machinery
Standard EN 60204: Safety of Machinery
Standard EN 294
Standard EN 50081-1
Standard EN 50081-2
ISO Standard 3744
ISO 11201 -1-2
EEC Standard 89-336
Standard EN 953
Standard EN 954/1
Standard EN 61000
For Slowbeer We have been designing microbreweries for over 20 years and have reached a level of development that meets our expectations, manufacturing various types of equipment, from the simplest, such as the Slowbeer 250 to the most sophisticated, such as the Slowbeer 500 Plus.
We continue to implement our equipment to provide brewers with new tools, improve thermal performance and energy savings.
Cheers!